
Views: 0 Author: Site Editor Publish Time: 2025-09-09 Origin: Site
Choosing the best polishing compound for stainless steel depends on the surface condition, polishing stage, and desired finish. Different compounds are designed for heavy cutting, scratch removal, intermediate polishing, or final buffing.
For stainless steel, black emery compounds are commonly associated with heavier cutting, white polishing compounds can be suitable for intermediate or finishing operations, and green rouge compounds are often selected for achieving a bright, mirror-like finish. However, actual performance varies with the compound formulation, buffing wheel, and polishing conditions.
This guide compares common stainless steel polishing and buffing compounds, explains their applications, and helps you choose the right compound and polishing wheel for industrial metal finishing.
There is no single polishing compound that works best for every stainless steel application. The right choice depends on whether you need to remove scratches, refine the surface, or achieve a mirror finish.
Polishing Requirement | Recommended Compound Type |
|---|---|
Heavy cutting and surface preparation | Black Emery or a suitable cutting compound |
Intermediate polishing | White Polishing Compound |
Mirror-like finishing | Green Rouge or a compatible fine finishing compound |
General stainless steel buffing | Stainless Steel Buffing Compound |
For the best results, match the polishing compound with the appropriate buffing wheel and use a progressive finishing process when the surface requires multiple stages.
Different stainless steel polishing compounds are designed for specific finishing stages, from removing surface scratches to achieving a high-gloss finish. Selecting the right compound depends on its abrasive properties, the workpiece condition, and the desired surface quality.
The following comparison highlights common polishing compounds and their typical applications in stainless steel finishing.
Polishing Compound | Cutting Ability | Typical Finish | Best Application |
|---|---|---|---|
Black Emery | High | Rough to intermediate | Heavy cutting, removing machining marks |
White Polishing Compound | Medium to High | Smooth, semi-gloss | Intermediate polishing and surface refinement |
Green Rouge | Low | High-gloss or mirror-like | Final buffing of stainless steel |
Greystar Compound | Medium to High | Smooth finish | Cutting and preliminary polishing, depending on formulation |
Stainless Steel Buffing Compound | Varies | Satin to high-gloss | General polishing and finishing |
Brown Tripoli | Medium | Smooth finish | Primarily softer metals; selected stainless steel applications if compatible |
Fine Finishing Compounds | Low | Bright, refined finish | Final polishing and removing fine finishing marks |
Note: Cutting ability and finish quality vary by manufacturer, abrasive formulation, polishing wheel, and operating conditions. The table represents general applications rather than standardized performance ratings.
For stainless steel surfaces with visible machining marks, a suitable cutting compound such as Black Emery may be used during the initial finishing stage. White polishing compounds can help refine the surface, while Green Rouge or another compatible fine compound is often used for final buffing.
For industrial stainless steel polishing, the compound should be selected together with the buffing wheel, polishing pressure, and required surface finish.
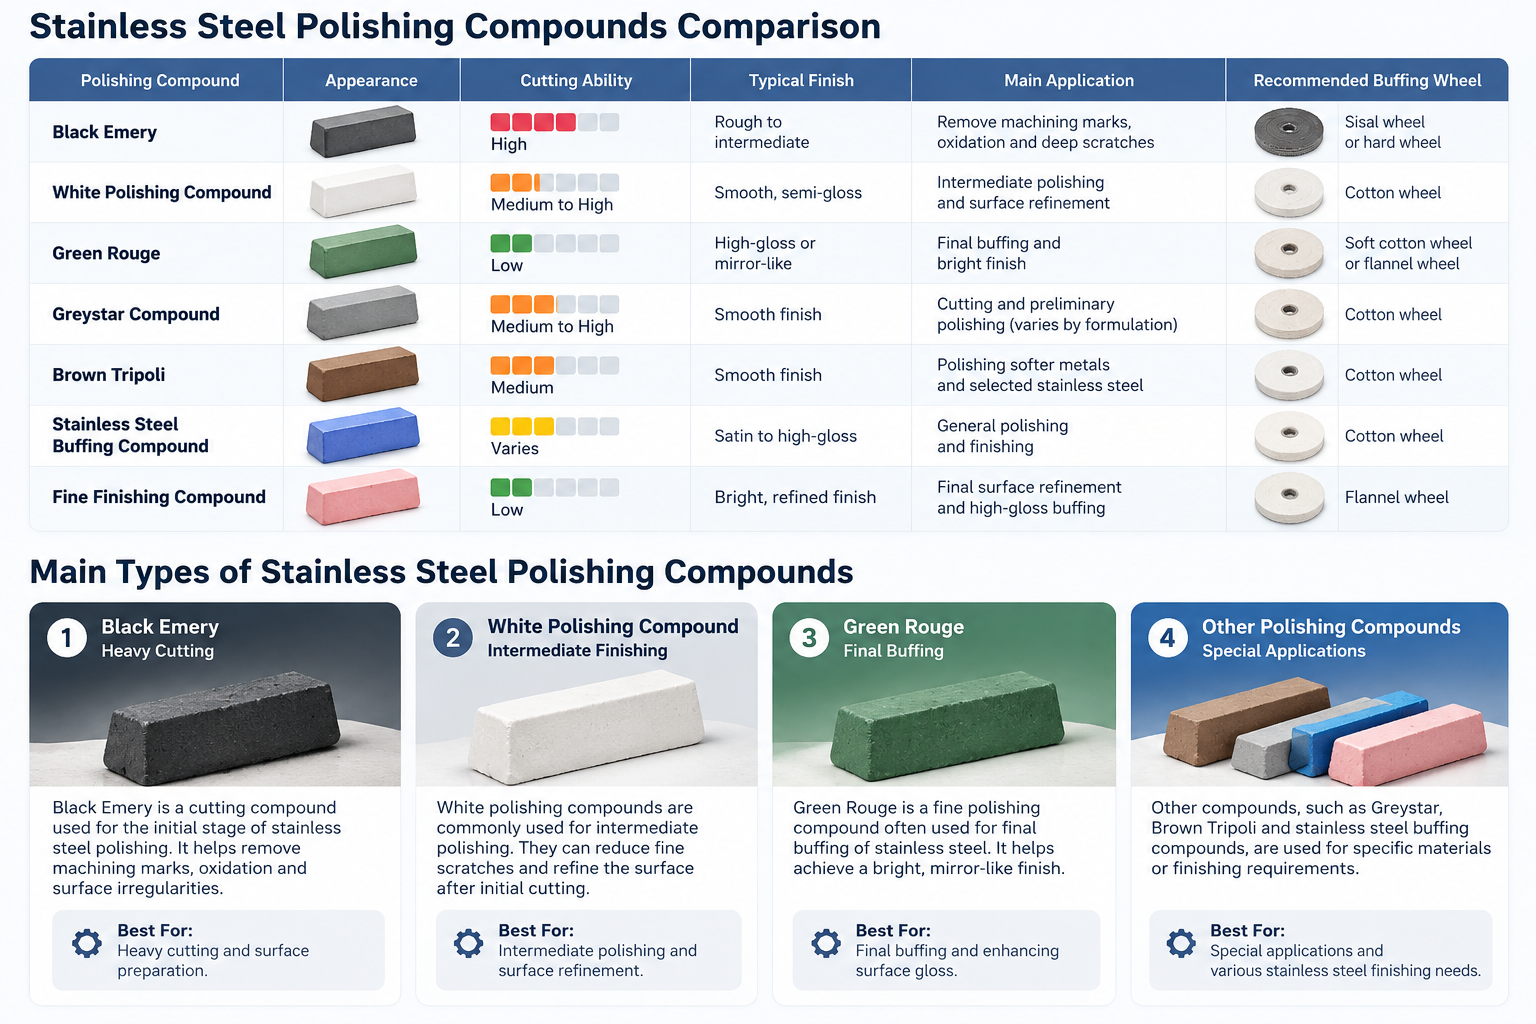
Stainless steel polishing compounds are available in different abrasive formulations for cutting, intermediate polishing, and final buffing. Their performance depends on the abrasive material, compound composition, buffing wheel, and polishing conditions.
Understanding the main types helps manufacturers select suitable compounds for different stainless steel finishing requirements.
It is generally used with suitable cutting wheels for preliminary stainless steel surface preparation.
Best For: Initial cutting, removing surface defects, and preparing metal for finer finishing.
They are often paired with appropriate cotton buffing wheels to produce a smoother, more uniform finish.
Best For: Intermediate polishing, reducing light finishing marks, and preparing surfaces for final buffing.
It is typically applied with soft buffing wheels after heavier scratches have been removed.
Best For: Final buffing, enhancing surface gloss, and achieving mirror-like stainless steel finishes.
Besides Black Emery, White Compound, and Green Rouge, manufacturers may use other formulations for specific materials or finishing requirements.
Compound Type | Typical Application |
|---|---|
Greystar | Cutting and preliminary polishing, depending on formulation |
Brown Tripoli | Commonly used for softer metals such as brass and aluminum |
Stainless Steel Buffing Compound | Formulated for cutting or finishing stainless steel, depending on grade |
Fine Finishing Compounds | Final surface refinement and high-gloss buffing |
Not all compounds are suitable for every stainless steel grade or polishing system. Always check the manufacturer's specifications and test the compound on sample workpieces before production.
Choosing the right stainless steel polishing compound requires considering the workpiece condition, desired surface finish, polishing equipment, and production requirements. A compound that works well for initial cutting may not be suitable for final mirror polishing.
Start by checking whether the stainless steel has machining marks, scratches, oxidation, or only minor surface imperfections. Heavy cutting compounds are generally suitable for initial material removal, while finer compounds are used to refine previously prepared surfaces.
Different finishing goals require different polishing approaches. A brushed or satin finish may require abrasive belt processing, while a mirror-like finish often involves progressive polishing and final buffing with a fine compound.
The buffing wheel affects cutting action, surface contact, and finishing quality. Sisal or treated cotton wheels are commonly used for more aggressive polishing, while softer cotton or flannel wheels are typically preferred for fine finishing. Always confirm compatibility with the selected compound.
For automated stainless steel polishing, consider workpiece geometry, polishing pressure, wheel speed, compound application, and production volume. Test the compound and wheel combination on sample parts before applying it to full-scale manufacturing.
| Surface Requirement | Suggested Compound | Typical Finishing Stage |
|---|---|---|
| Heavy machining marks | Suitable cutting compound, such as Black Emery | Initial cutting |
| Light scratches and dull surfaces | Compatible White Polishing Compound | Intermediate polishing |
| High-gloss or mirror-like finish | Green Rouge or another fine finishing compound | Final buffing |
| General stainless steel finishing | Formulated stainless steel buffing compound | Depends on compound grade |
Important: Compound colors and formulations are not standardized across manufacturers. Always verify the compound specifications and test the finishing result before production.
Choosing the right buffing wheel is just as important as selecting the correct stainless steel polishing compound. Different wheel materials and constructions affect cutting action, polishing pressure, heat generation, and final surface quality.
For industrial stainless steel polishing, harder wheels are generally used for initial cutting, while softer wheels are preferred for final finishing.
| Polishing Compound | Recommended Buffing Wheel | Main Application |
|---|---|---|
| Black Emery | Sisal or treated cotton wheel | Heavy cutting and surface preparation |
| White Polishing Compound | Spiral-sewn cotton wheel | Intermediate polishing and scratch refinement |
| Green Rouge | Soft cotton or flannel wheel | Final buffing and mirror-like finishing |
| Greystar Compound | Sisal or sewn cotton wheel, depending on formulation | Cutting and preliminary polishing |
| Stainless Steel Buffing Compound | Cotton or sisal wheel, depending on compound grade | General metal polishing |
| Fine Finishing Compound | Soft cotton or flannel wheel | Final surface refinement |
Note: These are typical combinations rather than universal compatibility rules. Always follow the compound and wheel manufacturers' recommendations.
1. Use Separate Wheels for Different Compounds
Avoid mixing coarse cutting compounds with fine finishing compounds on the same buffing wheel. Cross-contamination can introduce scratches during final polishing.
2. Control Polishing Pressure and Wheel Speed
Excessive pressure or unsuitable wheel speed can increase heat generation, cause uneven finishes, and accelerate wheel wear. Use operating parameters appropriate for the equipment and workpiece.
3. Test the Combination Before Production
Before polishing large batches of stainless steel parts, test the selected compound and buffing wheel on sample workpieces to confirm the required surface finish and process consistency.
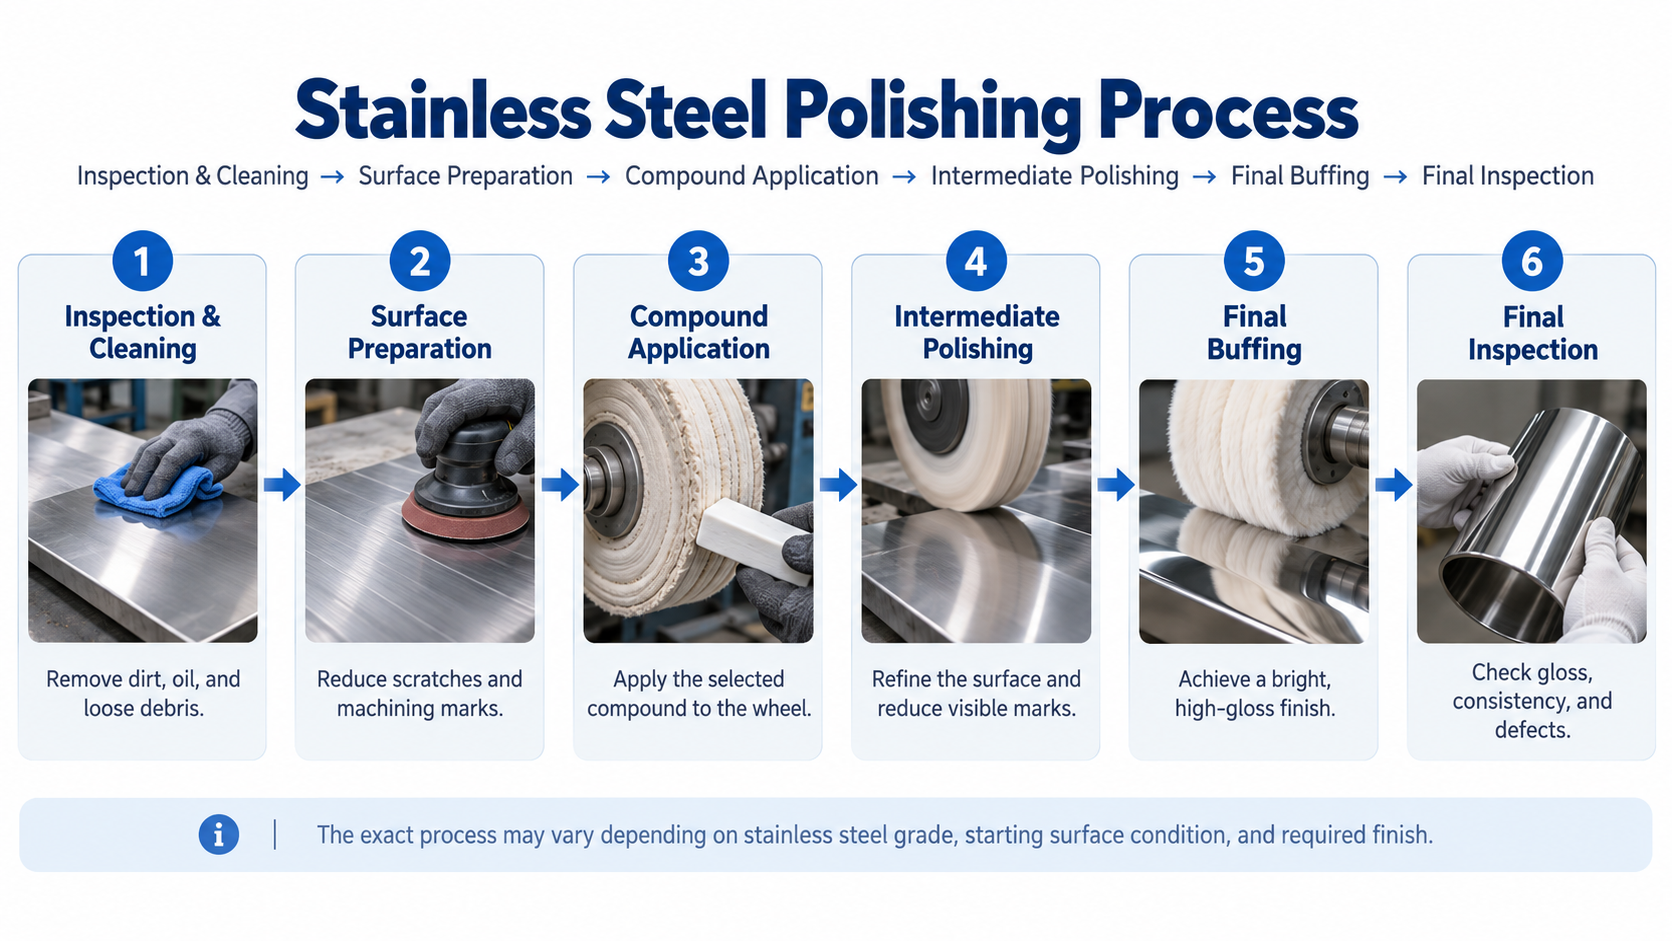
Polishing stainless steel requires proper surface preparation, suitable polishing compounds, and controlled finishing conditions. For industrial applications, the process typically progresses from removing surface defects to fine buffing, depending on the required surface finish.
Inspect the stainless steel workpiece for scratches, machining marks, oxidation, and surface contamination. Remove oil, dirt, and loose debris using a suitable cleaning method before polishing.
Use appropriate abrasive belts or cutting compounds to reduce visible machining marks and scratches. For heavily damaged surfaces, grinding or sanding may be necessary before compound-based polishing.
Choose a polishing compound according to the surface condition and finishing requirements. Apply a suitable amount to the compatible buffing wheel, following the compound and equipment manufacturers' instructions.
Use a suitable polishing wheel and compound to refine the surface and reduce marks left by earlier processing. Maintain controlled wheel speed, contact pressure, and workpiece positioning to improve finishing consistency.
For high-gloss applications, use a fine finishing compound such as a compatible Green Rouge formulation with a soft cotton or flannel wheel. Avoid contaminating the final buffing wheel with coarse cutting compounds.
Remove polishing compound residue using an appropriate cleaning method. Inspect the finished workpiece for remaining scratches, uneven gloss, and surface defects. If necessary, adjust the process and repeat the relevant finishing stage.
Note: Not every stainless steel component requires all six steps. The polishing sequence depends on the starting surface condition, material grade, and desired finish.
During stainless steel polishing, surface defects may still appear even when the correct compound and buffing wheel are used. Common issues include scratches, uneven gloss, polishing marks, and residue buildup. Identifying the cause helps improve polishing efficiency and final surface quality.
| Problem | Possible Causes | Recommended Solution |
|---|---|---|
| Deep scratches remain visible | Surface was not properly prepared; cutting stage was insufficient | Improve surface preparation and use a suitable cutting compound before final polishing |
| Uneven gloss or cloudy finish | Inconsistent polishing pressure, wheel wear, or improper compound use | Maintain stable polishing pressure, inspect the buffing wheel, and use a suitable finishing compound |
| Visible polishing marks | Coarse abrasives were not fully removed before the next stage | Use a progressive polishing sequence and clean the surface between stages |
| Compound residue on the surface | Excessive compound application or poor cleaning after polishing | Apply compound in controlled amounts and clean the workpiece thoroughly after each stage |
| Overheating or discoloration | Excessive pressure, wheel speed, or prolonged polishing in one area | Reduce pressure, adjust speed, and keep the polishing motion even |
| Final finish lacks mirror effect | Final buffing compound or wheel is not suitable for high-gloss finishing | Use a fine finishing compound, such as a compatible Green Rouge, with a soft cotton or flannel wheel |
To improve stainless steel polishing quality, manufacturers should control abrasive progression, use separate buffing wheels for different compounds, and test polishing parameters on sample parts before full production. Regular inspection of polishing wheels and cleaning of the workpiece between stages can also help reduce recurring defects.
Stainless steel polishing compounds are widely used in industrial metal finishing to remove surface imperfections, refine surface textures, and achieve consistent satin or mirror-like finishes. The combination of polishing compound, buffing wheel, and equipment should be selected according to the workpiece geometry, material, and finishing requirements.
Stainless steel pots, pans, kitchen utensils, and cookware components often require sanding and polishing to achieve smooth, decorative surfaces. Suitable polishing compounds can help reduce fine finishing marks and produce consistent satin or high-gloss finishes.
Common Finishing Processes: Sanding, Intermediate Polishing, Final Buffing
Stainless steel faucets, bathroom fittings, and sanitary hardware may require multiple finishing stages to achieve uniform surface appearance. Cutting compounds help prepare imperfect surfaces, while fine polishing compounds can enhance gloss on suitably prepared components.
Common Finishing Processes: Surface Preparation, Polishing, Buffing
Stainless steel door handles, locks, hinges, and decorative hardware often require controlled polishing to remove manufacturing marks and achieve consistent finishes. The appropriate compound and buffing wheel combination depends on the product shape and specified surface texture.
Common Finishing Processes: Grinding, Sanding, Polishing
Stainless steel exhaust components, decorative trim, and selected automotive hardware may require polishing to improve surface quality and appearance. Industrial polishing compounds are used alongside suitable buffing equipment to refine surfaces and achieve the desired finish.
Common Finishing Processes: Surface Preparation, Intermediate Polishing, Final Buffing
Selecting the appropriate polishing compound is only one part of achieving consistent stainless steel finishing results. The polishing machine, buffing wheel, workpiece positioning, and processing parameters also influence surface quality.
Yatai Polishing Machine Co., Ltd. provides automated grinding, sanding, and polishing equipment for industrial metal finishing applications.
Explore our solutions for Cookware & Kitchenware, Faucet & Sanitary Ware, Locks & Architectural Hardware, and Automotive & Motorcycle Parts to find equipment suited to different workpiece geometries and finishing requirements.
The best polishing compound depends on the surface condition and desired finish. Black Emery is commonly used for heavier cutting, white polishing compounds for intermediate finishing, and Green Rouge for final buffing. For industrial applications, always select a formulation compatible with the stainless steel grade, buffing wheel, and polishing equipment.
Polishing compounds and buffing compounds are closely related, and the terms are often used interchangeably. However, polishing compounds may refer to materials used throughout cutting and finishing stages, while buffing compounds often emphasize surface refinement and final shine. Their actual performance depends on the abrasive formulation rather than the product name.
Yes. Green Rouge is commonly used for final buffing of stainless steel, particularly when a bright or mirror-like finish is required. Many green formulations contain chromium oxide abrasives. However, compound colors are not standardized, so manufacturers should verify compatibility and test the product before use.
A fine finishing compound, such as a compatible Green Rouge, is often used with a soft cotton or flannel buffing wheel to achieve a mirror-like finish. Deep scratches and machining marks should be removed during earlier sanding and polishing stages before final buffing.
Yes, suitable polishing compounds can remove or reduce scratches depending on their depth and abrasive strength. Heavy cutting compounds help address more noticeable surface marks, while finer compounds refine the finish. Deep scratches may require grinding or sanding before compound-based polishing.
Sisal or treated cotton wheels are commonly used with cutting compounds, while sewn cotton wheels are suitable for many intermediate polishing operations. Soft cotton or flannel wheels are generally preferred for final buffing. The ideal combination depends on the compound formulation, workpiece geometry, and finishing requirements.
A single compound may be suitable for certain limited finishing tasks, but multiple stages often require different abrasive formulations. Initial cutting removes surface defects, intermediate polishing refines the surface, and final buffing enhances gloss. Using separate compounds and compatible wheels can improve finishing consistency and reduce cross-contamination.
Choosing the best polishing compound for stainless steel depends on the surface condition, required finish, and polishing process. Black Emery is commonly used for initial cutting, white polishing compounds for intermediate finishing, and Green Rouge for final buffing. However, actual performance varies with the compound formulation and buffing wheel selection.
For industrial manufacturers, achieving consistent stainless steel polishing results requires more than the right compound. Suitable polishing equipment, controlled processing parameters, and proper surface preparation are equally important.
Yatai Polishing Machine Co., Ltd. provides automated metal grinding and polishing solutions for various industrial applications. Explore our CNC Polishing Machines and Industrial Polishing Solutions to find equipment suited to your manufacturing requirements.


